
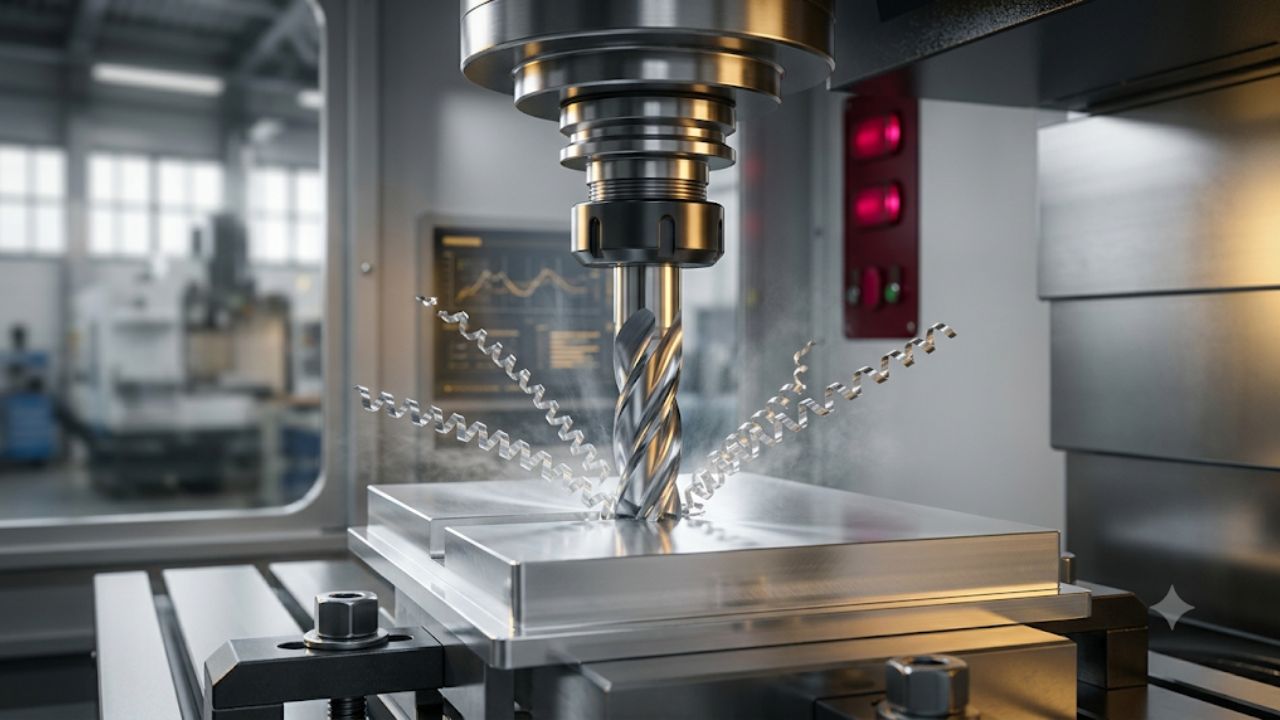
Aluminum is often described as easy to machine because it is softer than steel and supports high material-removal rates. Yet it creates large, sticky chips and may weld itself to a cutting edge when tool geometry or cutting data is wrong. An end mill that works well in steel is therefore not automatically suitable for aluminum.
The best end mills for aluminum machining combine sharp cutting action, generous chip space, smooth flutes, and adequate rigidity. The right tool improves finish, protects small features, and prevents built-up edge, chip packing, chatter, and broken flutes. This guide explains the main requirements for roughing, slotting, pocketing, finishing, and three-dimensional contouring.
Why Aluminum Needs Purpose-Built End Mills
Aluminum behaves differently from harder ferrous metals. Many wrought grades are relatively soft and ductile, so the material tends to form thick, continuous chips rather than short, brittle ones. Those chips need room to curl and leave the cut. If the flute valleys are too small, chips can become trapped, rub against the wall, and be cut again. That raises temperature and can damage both the tool and the finished surface.
Aluminum also has a strong tendency to adhere to a hot or dull edge. A small deposit can grow into built-up edge, changing the effective geometry of the end mill. The result may be a rough finish, oversize dimensions, burrs, or sudden edge chipping. Good aluminum tooling therefore aims to cut cleanly, move chips away immediately, and minimize friction.
Main Requirements for End Mills Used in Aluminum Machining
1. Sharp Cutting Edges and Positive Rake Geometry
A sharp edge is the first requirement. Aluminum-specific end mills normally use positive rake and enough clearance to shear instead of push or rub the material. Lower cutting forces help on thin walls, small parts, delicate workholding, and lower-power machines. The edge must still be strong enough for the selected feed and engagement, so a quality tool balances sharpness with a carbide grade and core that resist micro-chipping.
2. The Right Flute Count and Large Chip Gullets
Two- and three-flute designs are common because they leave large spaces between cutting edges. A two-flute tool maximizes chip capacity for full-width slots, deep pockets, and gummy grades. A three-flute tool can raise feed rate and improve finish while retaining useful chip space. Four- or five-flute aluminum tools may excel in light-radial-engagement milling, but they need controlled toolpaths and dependable evacuation. More flutes are not automatically better.
3. A Suitable High-Helix Design
Aluminum end mills often use a higher helix than general-purpose tools. A helix around 35 to 45 degrees is common, with some finishing tools going higher. This creates a smoother shearing action and can improve wall finish. It also raises axial force, so workholding and holder grip must be secure. In heavy roughing, balance helix, core strength, and flute volume rather than simply choosing the highest angle.
4. Polished Flutes and Low-Friction Surfaces
Polished or highly finished flutes reduce friction and make it harder for aluminum to stick to the tool. This is one reason aluminum-specific tools often look brighter and smoother than coated steel-cutting end mills. A smooth rake face helps chips slide away before they are compressed against the flute. Polishing is particularly valuable when machining gummy alloys, deep pockets, narrow slots, or parts where coolant access is limited.
5. Rigid Carbide Construction and a Strong Core
Solid carbide is widely used because it provides stiffness, wear resistance, and sharp geometry at high spindle speed. Deflection changes chip thickness and can leave tapered walls. The tool needs enough core strength without sacrificing too much flute space. Use the shortest flute length and projection that safely reach the feature; extra length increases bending and chatter.
6. An Appropriate Coating – or No Coating
Uncoated carbide is often excellent for wrought aluminum because it can be polished to a sharp edge. Coatings help when designed to reduce adhesion and friction, but a thick edge treatment can cause rubbing. For abrasive high-silicon cast aluminum or long production runs, wear-resistant, diamond-coated, or PCD tooling may justify the cost. Follow the supplier’s material recommendation rather than coating color or marketing terms.
7. The Correct End Profile and Corner Design
End shape must match the feature. Square tools produce flat floors, while corner-radius tools strengthen the edge for roughing or repeated production. Ball-nose tools suit molds and curved profiles, although cutting speed falls near the tip center. Chipbreaker roughers can shorten chips; finishing tools usually use continuous sharp edges for a smoother surface.
8. Low Runout and Secure Toolholding
Even the correct end mill will underperform in a worn collet or dirty holder. Low runout shares chip load evenly; otherwise one flute wears faster and leaves repeating wall marks. Clean the shank and holder, inspect the collet, use proper clamping length, and keep the collet away from the shank-to-flute transition. Secure the workpiece for high feed rates.
9. Effective Lubrication and Chip Evacuation
Chip evacuation is a tool-and-process requirement. The flute must have sufficient volume, but air blast, mist, minimum-quantity lubrication, flood coolant, or through-tool delivery may still be needed. The correct choice depends on machine enclosure, part geometry, alloy, depth, and workplace rules. Lubrication reduces adhesion, while directed air or coolant removes chips before they are recut. Deep slots and closed pockets need more attention than open side milling. If chips are collecting around the tool, increasing spindle speed alone will not solve the problem.
10. Compatibility With the Aluminum Alloy
The aluminum grade affects tool selection. Common wrought alloys such as 6061 are usually forgiving and work well with standard aluminum-specific carbide end mills. High-strength alloys such as 7075 can produce clean chips but may demand stable workholding and accurate cutting data. Softer sheet and marine grades can be more prone to smearing and built-up edge. Cast alloys with substantial silicon content are more abrasive and can wear a sharp carbide edge quickly. Before selecting a tool, identify whether the material is wrought, cast, high-silicon, anodized, or a metal-matrix composite.
Quick End Mill Selection Checklist
| Requirement | What to Look For |
| Cutting edge | Sharp, positive geometry that shears instead of rubbing |
| Flute count | Usually 2-3 for general work; more only with suitable engagement and evacuation |
| Flute space | Large polished gullets for bulky aluminum chips |
| Helix angle | High enough for smooth shearing, but balanced against axial force |
| Tool material | Rigid, fine-quality carbide for speed, accuracy, and edge retention |
| Coating | Uncoated polished carbide or a coating specifically rated for nonferrous alloys |
| Stickout | Shortest practical projection and flute length |
| Chip control | Directed air, mist, MQL, flood, or through-tool delivery as appropriate |
| Application match | Profile and geometry selected for slotting, roughing, finishing, or 3D work |
Matching the End Mill to the Operation
Tool geometry should also reflect how much of the cutter is engaged. The same end mill may behave very differently in a full slot and in a light finishing pass.
- Slotting and deep pockets: Choose fewer flutes, large polished gullets, and strong chip evacuation. Reduce axial depth or feed if chips cannot escape, and avoid repeatedly recutting chips at the bottom of the pocket.
- Adaptive or high-efficiency roughing: Three or more flutes can be productive when radial engagement is low, toolpaths maintain a consistent load, and the machine can supply the programmed feed. A corner radius can improve edge strength.
- Side finishing: A sharp high-helix tool with low runout and suitable flute length can produce a clean wall. Leave a controlled amount of stock for the finishing pass rather than rubbing over a nearly finished surface.
- Three-dimensional contouring: Use ball-nose or tapered ball-nose tools for curved shapes. Program stepovers according to the required cusp height and remember that cutting speed changes across the ball.
- Thin walls and delicate features: Use sharp tools, light radial engagement, balanced passes, and minimal tool projection. Alternate sides or use staged finishing so cutting pressure does not bend the feature.
Speeds, Feeds, and Chip Load Still Matter
Aluminum usually allows higher cutting speed than steel, but spindle speed is only one part of the process. The end mill must take a real chip. If feed per tooth is too low, the edge rubs instead of cutting, creating heat and encouraging aluminum to smear onto the flute. If chip load is too high for the tool diameter, stickout, or engagement, the cutter may deflect or break. Start with the tool maker’s data for the exact diameter, flute count, alloy group, and operation, then adjust while watching spindle load, chip shape, sound, finish, and temperature.
Feed rate depends on spindle speed, flute count, and chip load per tooth. A three-flute tool can achieve more feed than a two-flute tool when chip space remains adequate. During light radial cuts, compensate for chip thinning so actual chip thickness does not become too small. Program entries, corners, and slot sections to avoid sudden load increases.
Common Aluminum Milling Problems and Practical Fixes
Most poor results can be connected to a small group of tooling or process mistakes.
- Built-up edge: Use a sharper aluminum-specific tool, confirm lubrication, increase chip load from a rubbing condition, improve chip removal, and replace a worn cutter.
- Chips packing in flutes: Select fewer flutes or larger gullets, shorten the depth of cut, add directed air or coolant, and use a toolpath that gives chips an exit path.
- Rough walls or dimensional taper: Reduce tool projection, inspect runout, use a stiffer end mill or holder, decrease radial load, and add a separate finishing pass.
- Burrs at the top or bottom edge: Check cutting-edge sharpness, feed direction, part support, and exit strategy. A finishing pass or edge-strengthening corner geometry may help.
- Chatter: Improve rigidity, vary spindle speed, reduce unsupported length, choose a variable-helix or variable-pitch tool when appropriate, and avoid unstable combinations of axial depth and radial engagement.
How to Evaluate an End Mill Supplier
A suitable end mill is more than a diameter and flute count. Review the tool’s recommended material group, helix, rake, core size, usable length, corner design, coating, and cutting-data range. Reliable product information should explain whether the tool is intended for slotting, roughing, finishing, or dynamic milling. In professional CNC machining, the tool, holder, machine, coolant method, program, and workholding must operate as one system.
When comparing a manufacturer, look for clear dimensional data, consistent edge preparation, traceable carbide quality, application support, and realistic speeds-and-feeds guidance. A cheaper general-purpose cutter may cost more through slow cycle times, scrapped parts, and frequent tool changes. The best value is the tool that delivers predictable part quality and cost per component.
Tool Care and Replacement
Inspect the end mill before critical work because aluminum deposits can hide damage. Clean it with a method approved for the coating and avoid scratching polished flutes. Keep holders and collets clean, store cutters separately, and track tool life by alloy and operation. Replace the cutter before finish or dimensions become unstable.
Frequently Asked Questions
What flute count is best for aluminum?
For most general work, a two- or three-flute carbide end mill designed for nonferrous materials is a strong starting point. Two flutes maximize chip space, while three flutes can provide a useful balance of evacuation, finish, and feed rate.
Should aluminum end mills be coated?
Not always. Uncoated, polished carbide is often ideal because it keeps the edge sharp. A coating is useful when it is engineered for low friction, adhesion resistance, or abrasive aluminum alloys. Use the supplier’s material recommendation.
Can a standard steel end mill cut aluminum?
A steel end mill may cut aluminum, but its flute count, edge preparation, coating, and chip space may cause rubbing or chip packing. For repeatable production and good finishes, aluminum-specific geometry is usually the safer choice.
Does a higher helix angle always improve machining?
A high helix improves shearing action and can create smoother walls, but it also increases axial force. Tool pullout resistance and workholding must be adequate, especially during aggressive cuts.
Why does aluminum stick to an end mill?
Common causes include dull edges, insufficient feed per tooth, poor lubrication, trapped chips, excessive heat, and unsuitable flute geometry. Correcting the cutting action and evacuation is more effective than simply lowering every parameter.
Conclusion
Aluminum machining requires end mills that cut sharply and clear chips without allowing the material to stick. The most important features are positive cutting geometry, adequate flute space, a suitable helix angle, polished surfaces, rigid carbide construction, low runout, and an end profile matched to the operation. Coating, coolant, flute count, and cutting data must also suit the exact alloy. By treating tool selection as part of the complete machining system, shops can run faster while protecting surface finish, accuracy, and tool life. More practical manufacturing and engineering guidance is available through aelftech.com.
Leave a Reply